

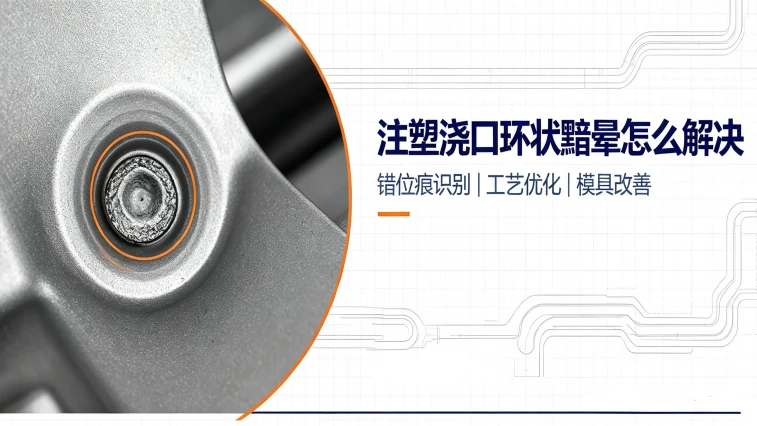
During precision injection molding mass production, many appearance parts show a typical defect: a ring-shaped dull halo forms around the gate, commonly called gate smear or gate halo in the industry. This color-difference defect directly affects the appearance grade of products and, in severe cases, directly causes batch defects, raw material loss and delivery delays. It is widely seen in the production of home appliance housings, 3C accessories, daily necessities and automotive appearance plastic parts.
I. Defect Phenomenon
A highly recognizable ring-shaped dull halo forms around the gate opening, with dark and uneven color. It is a surface flow-mark defect caused by the imbalance of melt shear and cooling, and is especially prominent in transparent materials and high-gloss appearance plastic parts.
II. Core Cause Analysis
Imbalanced process parameters: injection speed too high causes intense shear when the melt passes through the gate; barrel temperature too low results in insufficient melt fluidity; mold temperature too low causes the melt to rapidly form a solidified layer when contacting the mold wall, and the sliding of the flowing skin layer produces color differences.
Insufficient plasticizing conditions: back pressure set too low, uneven material mixing, poor melt consistency, aggravating molecular orientation disorder.
Mold structure design defects: lack of smooth transition at the junction between the gate and the product cavity, with step changes; gate diameter too small, further amplifying the shear rate; unreasonable gate opening position; sharp corner turns inside the product, disturbing the melt flow pattern.
III. Targeted Improvement Countermeasures
Process Optimization Plan
Adopt a multi-stage injection curve: slow → fast → fast; when the melt reaches the gate stage, fill at low speed to weaken the instantaneous shear impact at the gate;
Moderately raise the barrel temperature to improve melt fluidity;
Reasonably increase the back pressure to strengthen the uniformity of plasticizing and mixing;
Raise the mold wall temperature to delay the rapid cooling of the melt surface layer and release internal stress.
Mold Structure Optimization Plan
Add a smooth arc transition at the junction between the gate and the product to eliminate the flow-transition step;
Moderately enlarge the gate diameter to reduce the melt shear intensity;
Evaluate and adjust the gate opening position;
Change the sharp corners of the product into arc transitions to stabilize the melt flow front.
IV. Konger Machinery | Helping to Permanently Solve the Gate Smear Problem from the Equipment Side
Ningbo Konger Machinery Co., Ltd. is deeply engaged in the R&D and manufacturing of injection molding equipment. Relying on years of front-line molding commissioning experience, it provides equipment + process integrated solutions for appearance defects such as gate halo and gate smear.
✔ Intelligent segmented injection control system: Konger injection molding machines are equipped with a high-performance closed-loop control system, supporting refined multi-stage injection curve editing, accurately realizing low-speed buffer filling at the gate position, and controllably adjusting the injection speed of each stage, effectively reducing shear stress in the gate area and reducing ring-shaped halos from the process source.
✔ High-precision stable temperature control system: the equipment adopts independent PID segmented temperature control with small barrel temperature fluctuation; combined with a stable hydraulic and servo system and mold temperature process optimization recommendations, it ensures uniform and stable melt temperature, improves melt fluidity, and avoids the rapid surface solidification problem caused by low temperature.
✔ Customized plasticizing unit optional configuration: for high-gloss, transparent and engineering plastic scenarios, a low-shear optimized screw solution can be provided to improve melt homogenization and reduce appearance color-difference defects caused by poor plasticizing.
✔ Supporting molding technical support service: Konger has a professional team of process engineers who can provide customers with trial-molding process guidance, mold flow analysis suggestions, and gate and runner optimization references, helping customers quickly complete defect rectification, shorten commissioning cycles, improve product yield and reduce scrap costs.
Injection appearance defects are often the result of the combined action of process, mold and equipment. Choosing an injection molding machine with stable performance and excellent control precision, combined with scientific parameter commissioning and reasonable mold design, is the way to permanently solve appearance problems such as gate smear. For machine selection and process technical consultation, please contact Ningbo Konger Machinery.