

A nozzle that does not sit concentric with the sprue bush is the step most often waved through during commissioning: it looks centred, but it is a few tenths of a millimetre off — and that shows up as leaking at the contact face, an unstable cushion, and one-sided wear on the sprue bush. This article walks through the datum, the measurement, the adjustment and the hot-state re-check.
1. Sort Out the Three Datums First
1.1 The locating ring is the datum
The mold locating ring seats in the centre hole of the fixed platen, and that is what fixes the mold's position in the machine. The nozzle must align to the centre of the locating ring, not to whatever looks close on the platen face. The locating ring bore and the sprue bush outside diameter normally run with a 0.05–0.15 mm clearance — that clearance is one source of the alignment tolerance you are allowed.
1.2 What eccentricity costs
Leaking at the contact face: the two faces are not parallel, melt extrudes through the gap, and purging becomes a constant chore.
Unstable cushion: feed resistance varies with the offset, part weight drifts, and no amount of parameter tuning quite settles it.
Mechanical damage: the sprue bush wears on one side, the nozzle tip gets pushed out of straight, the injection-unit guideways take a side load — and the offset grows over time.
1.3 How close is close enough
Standard machines: ≤0.2 mm is the pass line. Precision thin-wall parts and small gates (≤φ2 mm): ≤0.1 mm. Hot-runner and pinpoint-gate molds are tighter still — follow the mold maker's tolerance.
2. Preparation Before You Touch Anything
Lock out and tag out, release hydraulic pressure, and let the nozzle and barrel cool — for safety, and so heat does not distort cold-state readings.
Remove the nozzle guard and heater band if needed, to expose the nozzle outside diameter as a measuring surface.
Clean the locating ring bore, the sprue bush outside diameter and the nozzle face. Residue and oil will falsify the dial reading.
Confirm the mold is clamped and the locating ring is fully seated in the platen hole — otherwise you are measuring a false centre.
3. How to Measure: Three Methods That Cross-Check
3.1 Dial indicator (first choice)
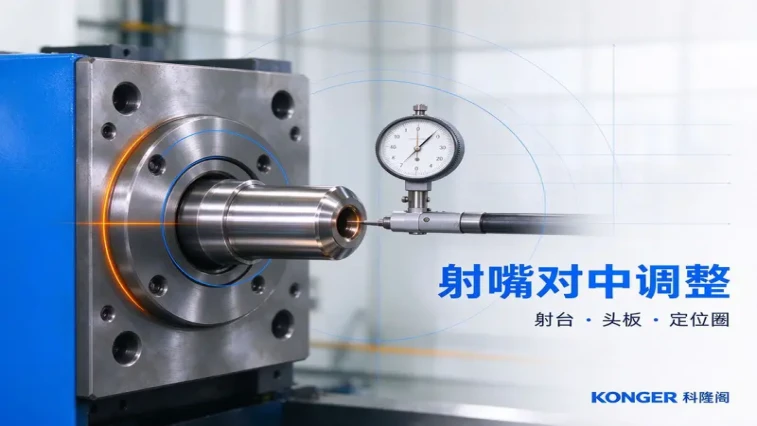
Mount a magnetic base on the fixed platen or the mold's fixed half, and touch the indicator to the nozzle outside diameter about 10–20 mm back from the tip. Read four points — top, bottom, left, right: the left/right difference is the X offset, the top/bottom difference is the Y offset. Keep the same indicator preload each time, make sure the base is rigid enough not to deflect, and keep the stylus clear of heater-band wiring. Four points catch taper and ovality that two points miss.
3.2 Imprint method (quick field check)
Place thin paper, or a light coat of red lead, on the sprue bush face, then bring the nozzle in slowly with light contact and see whether the imprint is centred and even. Fast, useful as a first call, not as acceptance.
3.3 Feeler gauge and eye
With the nozzle against the bush, run a feeler gauge around the contact: the gap should be even. If one side takes the gauge and the other does not, it is off-centre. The nozzle cone shape makes this easy to misread, so use it only as a support check.
4. Which Way to Move It
4.1 Lateral offset
Slacken the lock nut and bring the lateral adjusting screw in step by step against the dial reading, re-measuring after each move — do not chase it to zero in one pass. With clearance in the guideways the screw travel and the reading are not exactly 1:1, so it is a move-and-measure loop.
4.2 Height offset
Add shims or a wedge between the injection unit and the frame: shim up, remove to come down, with the wedge giving finer resolution. Changing height alters how the unit sits on its guideways, so check that forward and backward travel still runs free and without binding.
4.3 Nozzle droop
A long overhanging nozzle droops more. Check the front support and guideway wear first; if the structure is sound, leave the nozzle centre slightly above the datum when cold, then set the final value after the hot-state re-check.
4.4 Re-check after tightening
Tighten all bolts in diagonal sequence, in two or three stages, to the specified torque. Tightening alone moves things by around 0.05 mm, so re-indicate afterwards and fine-tune again if needed. A cold reading taken before tightening is not a result.
5. Hot-State Re-Check: The Step Everyone Skips
Cold alignment can be perfect; once the nozzle reaches working temperature it grows axially and the tip lifts or droops, taking the centre with it. Heat to the actual production temperature, hold for 20–30 minutes, then re-measure with the nozzle in contact and correct the cold allowance. Long nozzles and high-temperature materials (PA, PC, PET) move most — hot-state acceptance is mandatory there.
6. Where the Konger Design Helps
Common datum machining: on the K-TEC series (K-TEC120, K-TEC170, K-TEC1200 and others) the platen locating bore and the injection-unit centreline are machined to the same datum, and the locating-ring seating face is clean, so cold alignment starts from a trustworthy base.
Thicker platen, less deflection: the short clamping-force path keeps the platen from warping over years of running, so the alignment holds instead of drifting two months later.
Linear guideways on the injection unit: travel is smooth with little side clearance, so a lateral adjustment does not spring back and tightening moves the reading less.
Dedicated platforms: PET preform, artificial flower, TPR soft compound and flame-retardant nylon configurations match nozzle bore and sprue bush to the part, cutting the risk of forcing a general-purpose nozzle onto a small gate. CMS two-color and sandwich machines use parallel twin injection units with a shared nozzle, which demands tighter alignment at assembly and commissioning.
Service side: Konger includes alignment and trial-shot guidance in the installation handover, rather than leaving it at "it shoots a part, so it's fine".
7. Quick Field Checks
Constant leaking at the contact face: check alignment and face parallelism first, then nozzle temperature and back pressure.
Centre off again after a mold change: usually the mold's own locating ring and sprue bush are not concentric, or the ring is worn — the problem is in the mold, not the machine.
Drifts again after running a while: check injection-unit lock bolts, guideway wear and platen thermal distortion.
Erratic dial readings: base not rigid, residue on the measuring surface, or the unit creeping as it moves.
Conclusion
Nozzle alignment is not "move the nozzle until it looks centred". It is making three centrelines coincide — nozzle axis, locating ring centre, sprue bush centre — and keeping them coincident when hot. Cold indication, re-check after tightening, hot-state acceptance: all three, or it is not done. Konger's approach to platen datums, injection-unit guideways and dedicated platforms exists to keep that alignment from drifting in production.