

Causes and Solutions for Bubble Defects in Injection Molded Products
It aims to provide customers with professional and practical guidance on troubleshooting and resolving bubble defects in injection molded products.
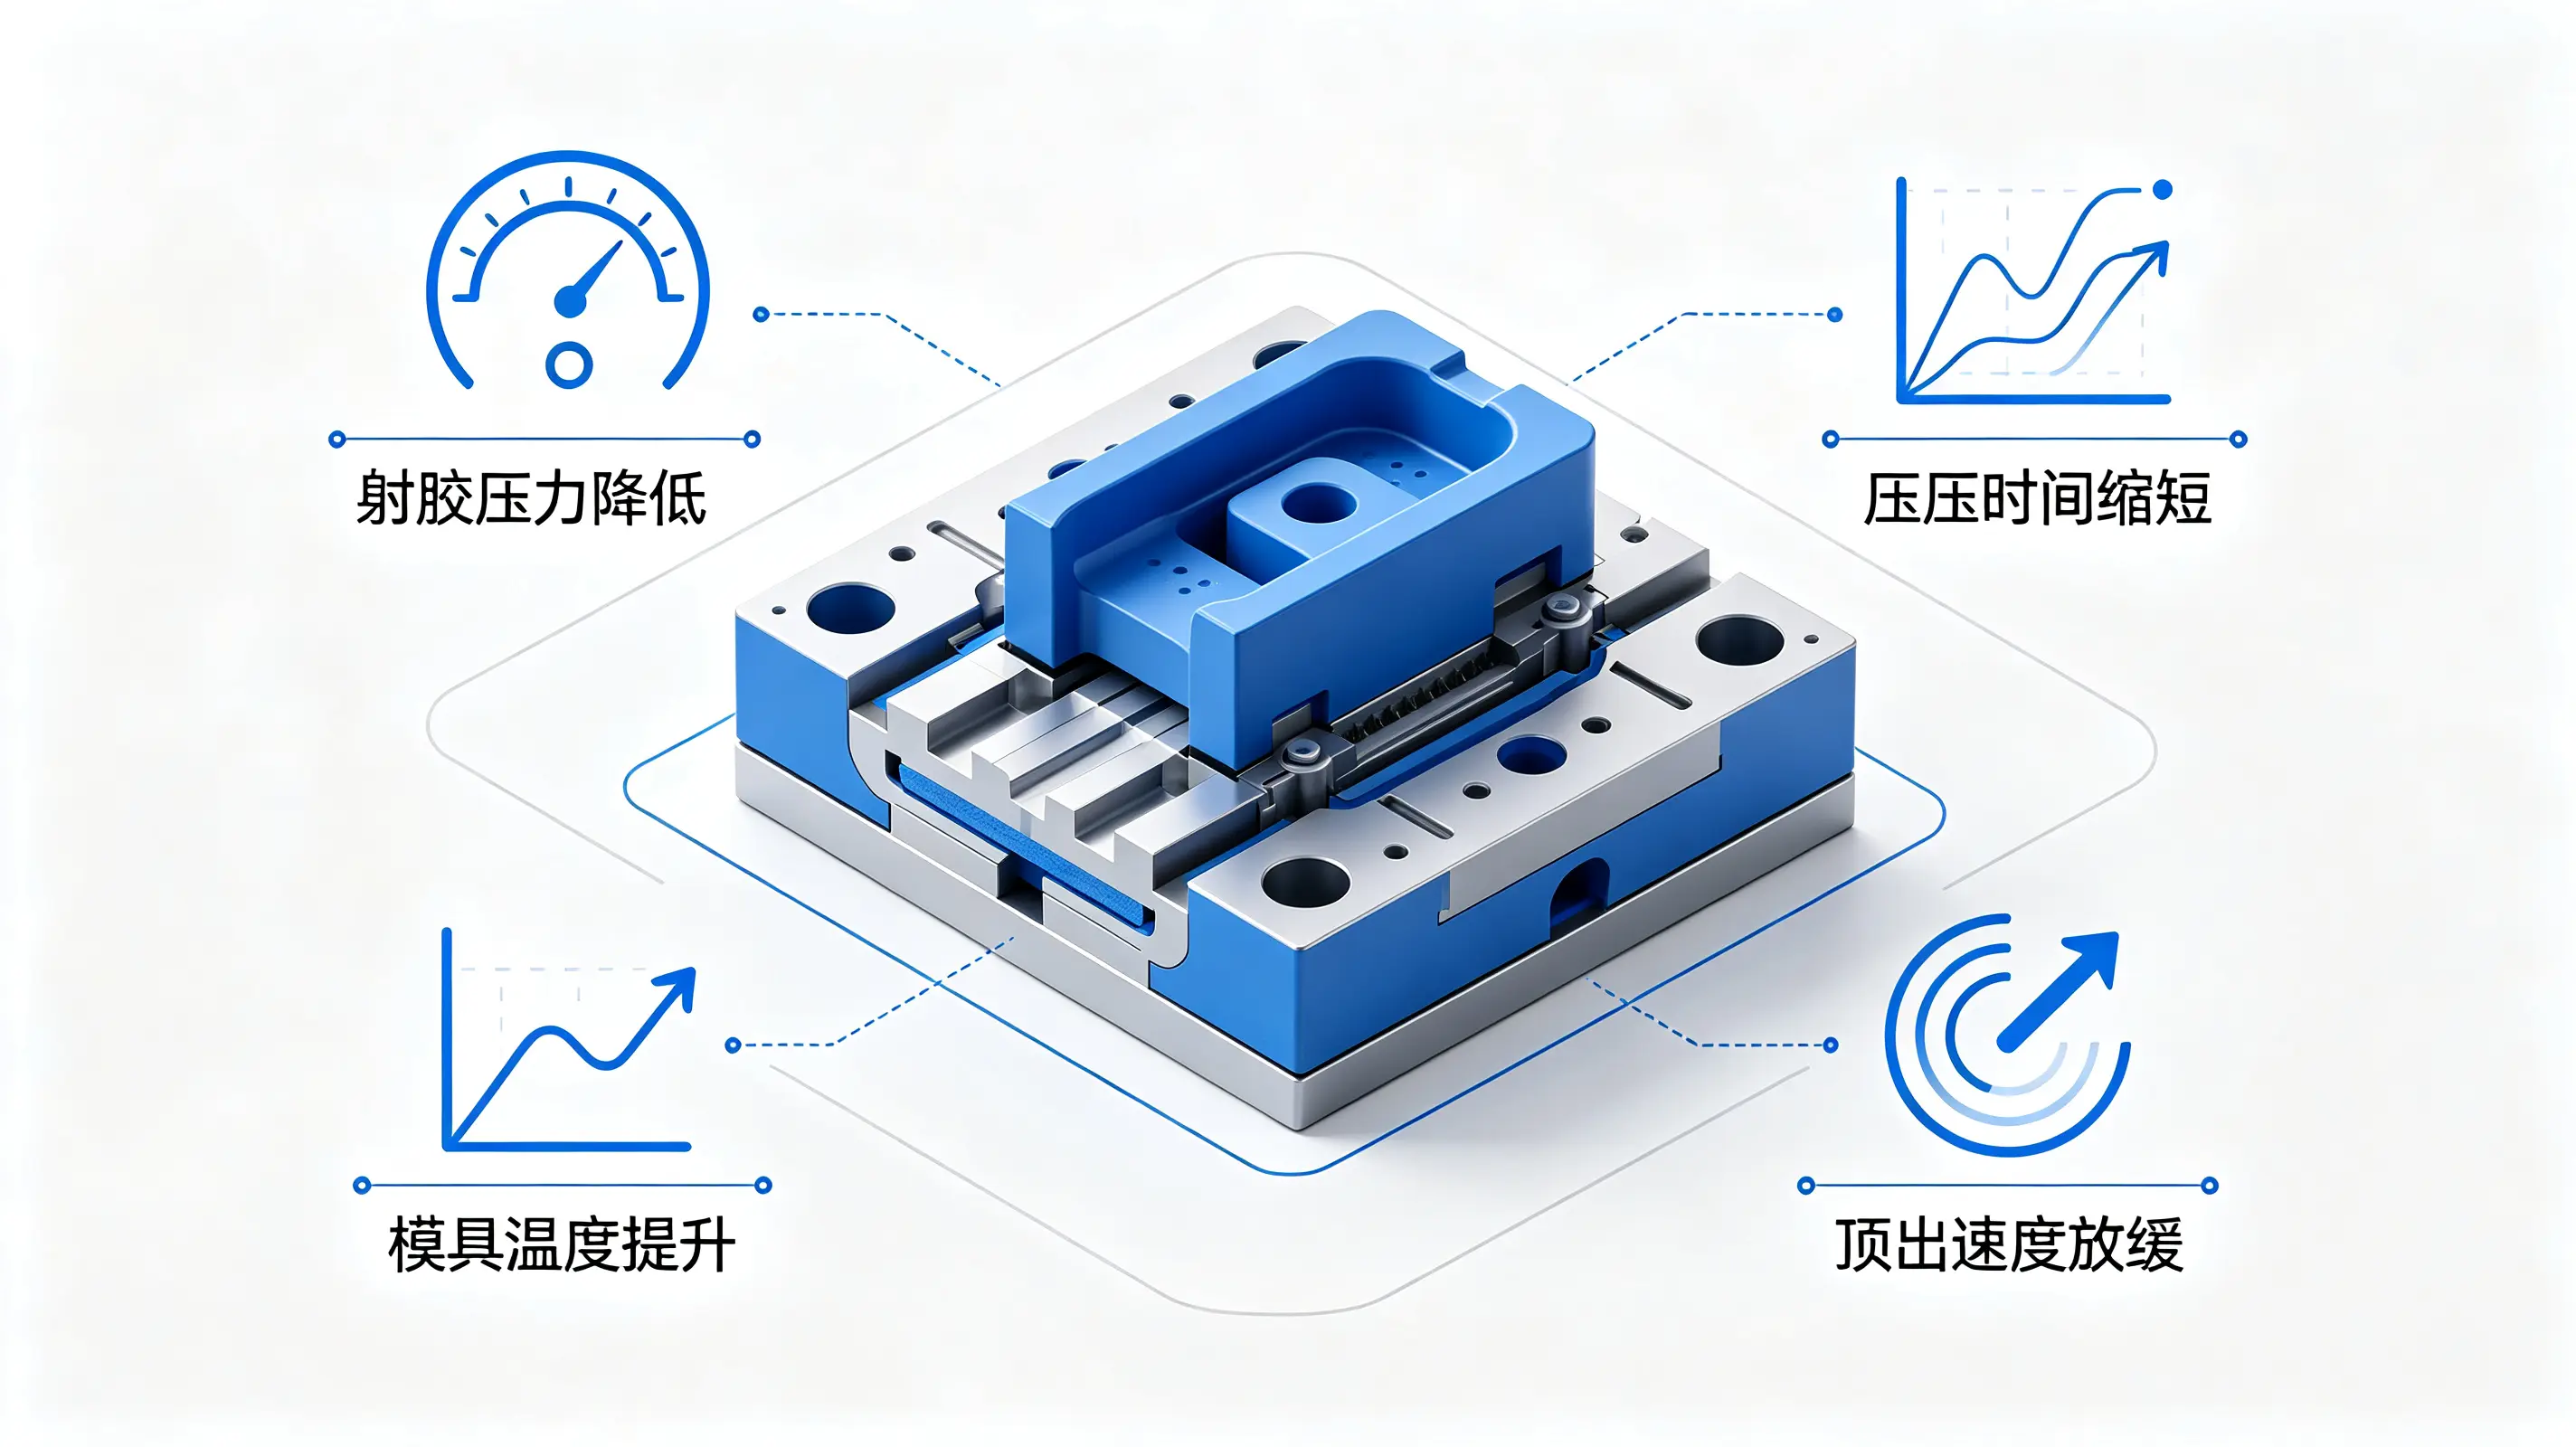
Difficult Demolding of Injection Molded Products | Causes and Solutions for Parts That Are Hard to Eject After Mold Opening
After mold opening, the product is stuck on the core or cavity and cannot be smoothly ejected, which easily causes part scratches, ejector white marks, cracking and deformation, and in severe cases, ejector pin breakage and mold damage, directly reducing production yield and lengthening the molding cycle, bringing shutdown losses and rising production costs to the enterprise. The essence of difficult demolding is that the shrinkage grip force and frictional resistance generated by the plastic part on the mold after cooling shrinkage are greater than the effective ejection force the equipment ejection system can provide. The fault sources span injection molding process...
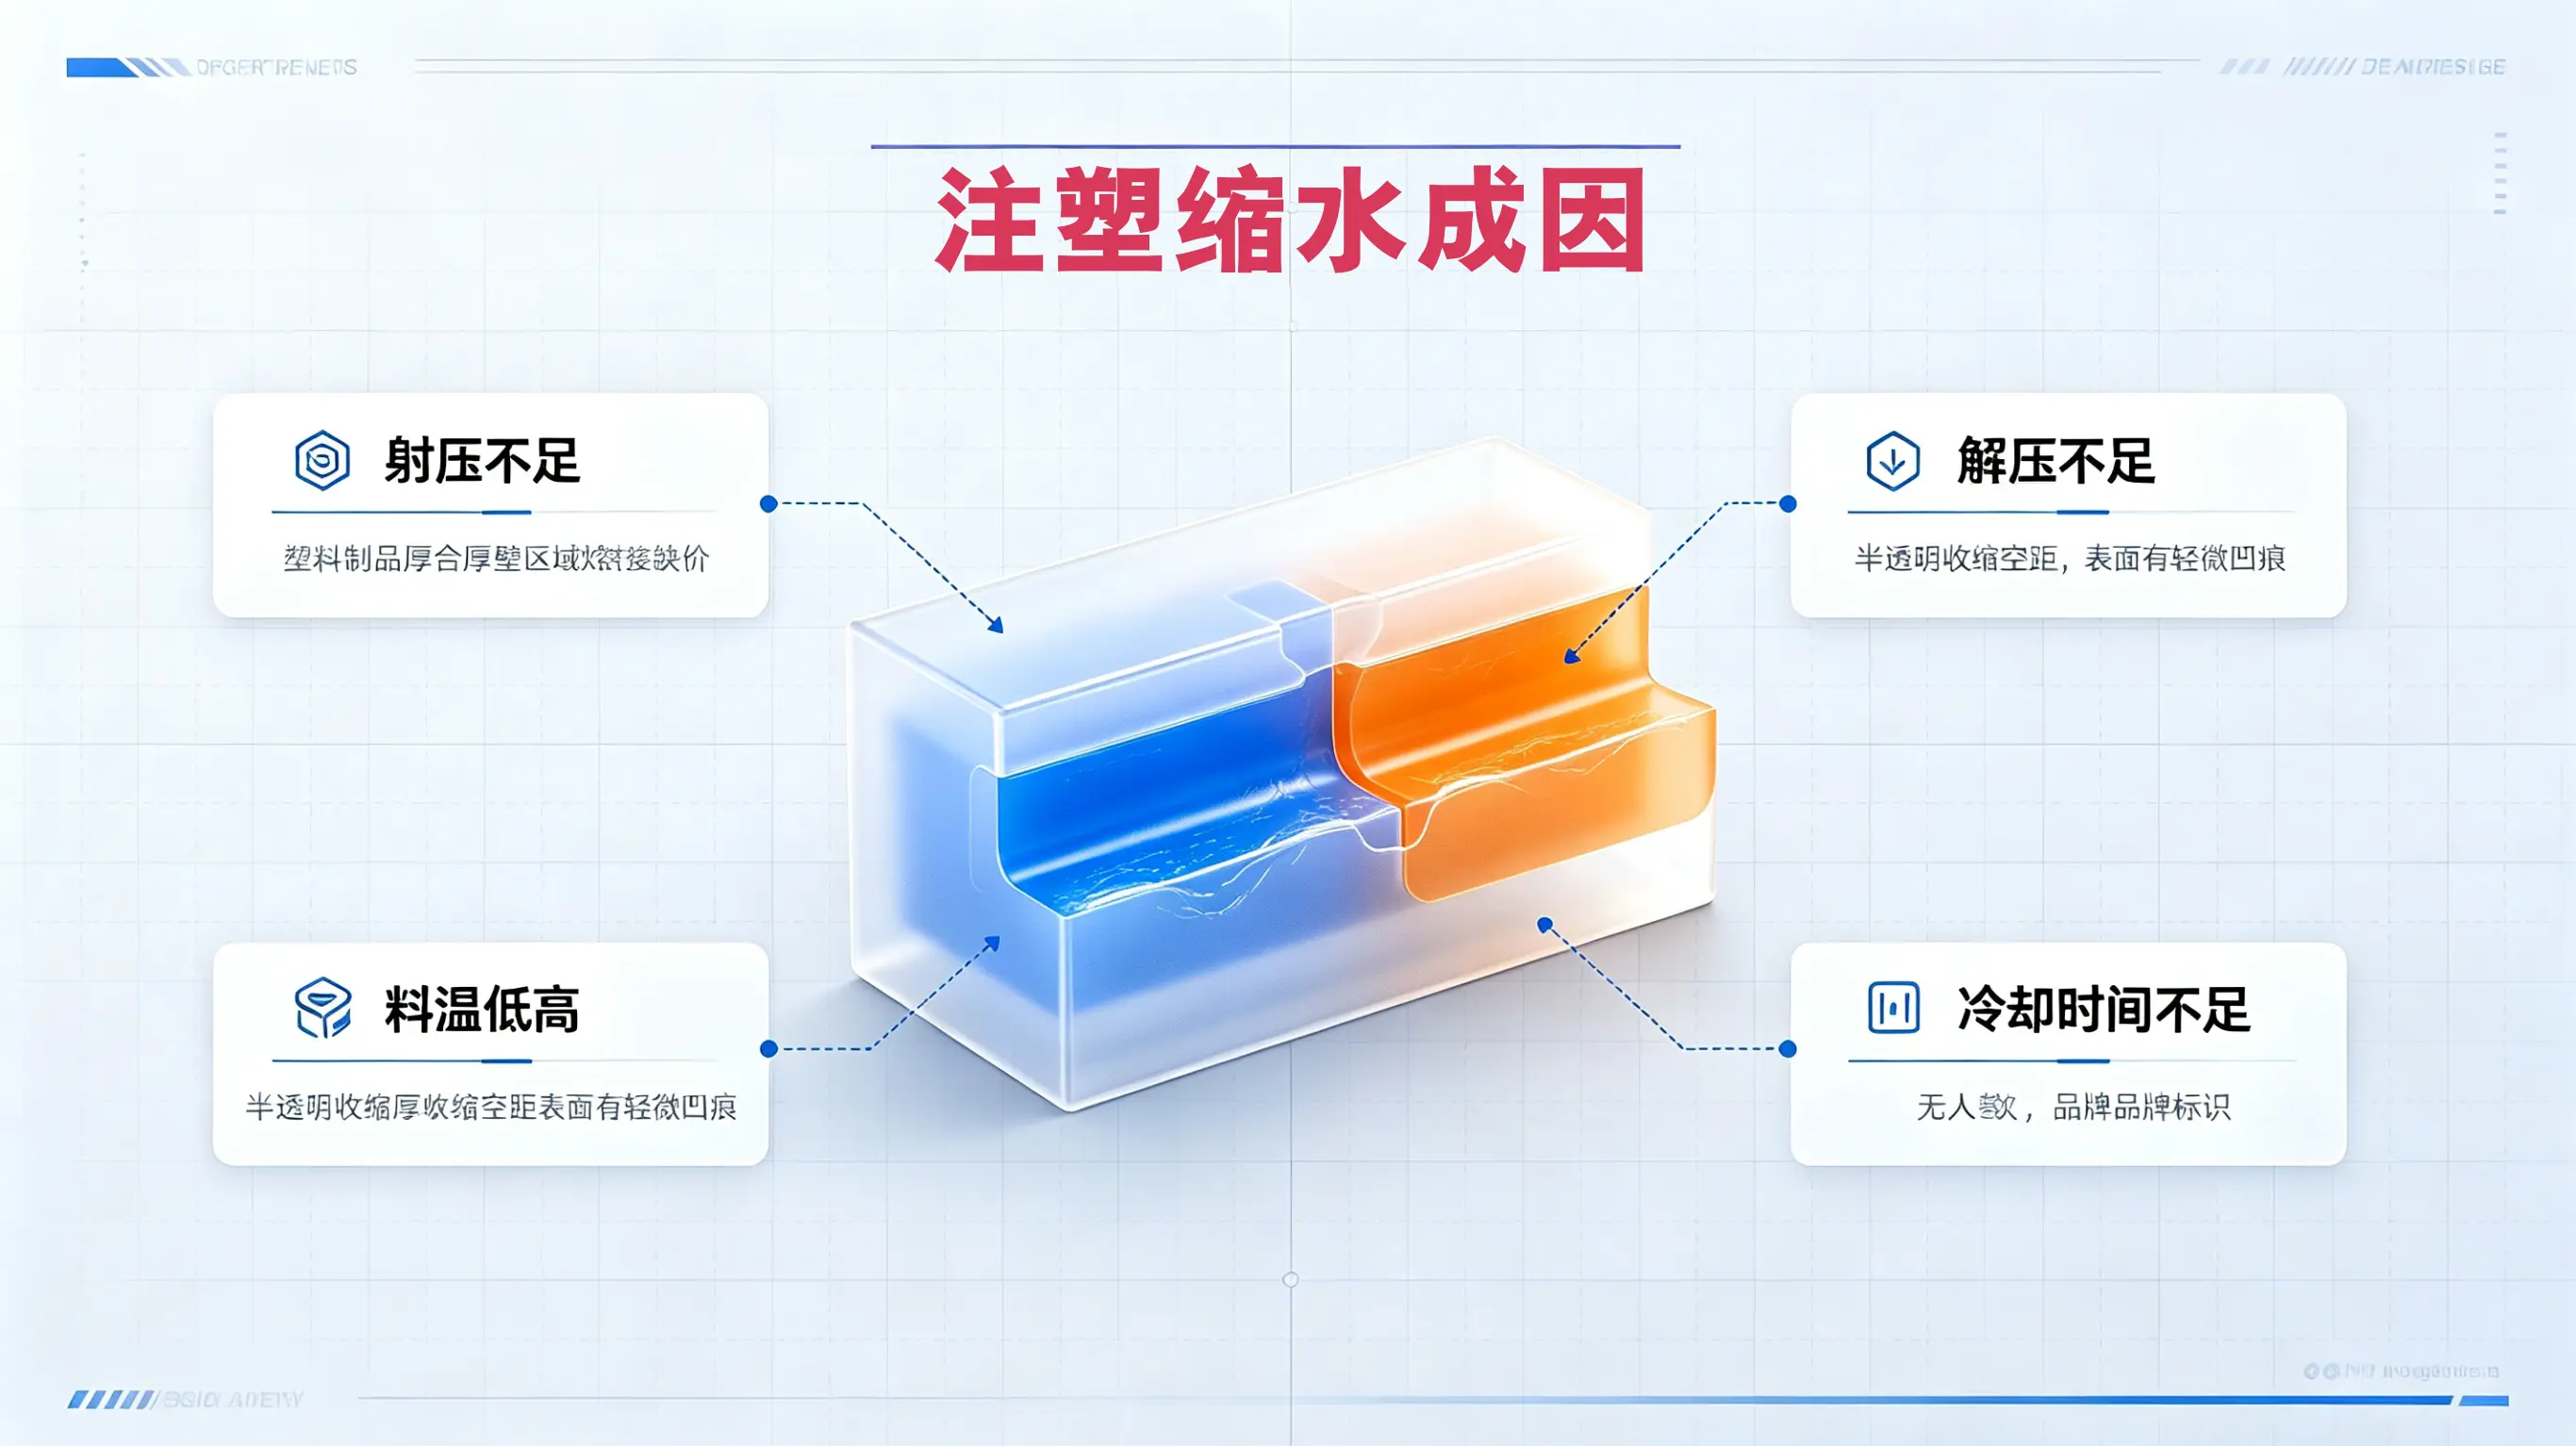
Analysis of the Causes of Product Shrinkage in Injection Molding and Solution Interpretation
Ningbo Konger Machinery has long been deeply engaged in the R&D of high-end injection molding equipment and the optimization of precision injection molding processes. Relying on a large number of on-site commissioning cases and equipment technical accumulation, it has completed multi-dimensional root-cause analysis of injection shrinkage defects, forming standardized solutions covering process, equipment, mold and raw materials, helping injection molding enterprises precisely solve shrinkage defects and stabilize mass production quality, reasonably extend cooling time, ensure products are fully cured and set before demolding, and avoid secondary shrinkage indentations in the later stage.